How Is AI Used in Manufacturing?
AI in manufacturing is software that learns from machine and sensor data to predict failures before they stop a line, inspect every product as it passes, tune process settings, and plan what to make next. It does not replace the machines. It learns their patterns and warns people early.
Picture a bearing on a night shift. A vibration sensor spots its pattern change at 3 a.m. on a Tuesday, the system flags it, and the crew swaps the bearing on the planned break.
The line never stops. No drama, no emergency callout.
That quiet save is what most factory AI actually looks like. This GuideAITools guide covers the main uses, the data each needs, the benefits plants report, and the limits vendors skip. The failures get their own section, because that is where the money leaks.
What Is AI in Manufacturing?
In plain words, AI in manufacturing is software that learns patterns from factory data and uses them to predict, inspect, decide, or adjust. It sits on top of the machines and control systems a plant already runs.
Four families do most of the work. Machine learning finds patterns in numbers, computer vision reads images, robotics acts on what the models see, and optimization software picks the best plan from many options.
Older automation follows fixed rules a programmer wrote once. AI systems adjust their calls as new data arrives, so their strength is learned patterns, not fixed rules. That is their weakness, because bad data teaches bad lessons.
You will hear this grouped under Industry 4.0, the name for connected, data driven factories. If the base idea is new to you, start with what artificial intelligence is and come back.
At GuideAITools, we count a tool as factory AI only when it learns from plant data. A timer that stops a conveyor every hour is automation. A model that learns which vibration pattern comes before a failure is AI.
How AI in Manufacturing Works: Sensors, Data, Decisions
Every factory AI system runs the same five step loop. Sensors capture signals from machines. The data gets cleaned and stored.
A model scores it or makes a prediction. Then a person or a controller acts, and the result feeds back into the model.
Vibration, temperature, motor current, spindle load, cycle counts, and camera images tell the story of a machine before it breaks. Machine learning is the part that learns which combinations of those signals matter.
A camera checking parts at line speed needs its answer in milliseconds, so that call happens on an edge device at the machine. Training on months of history is heavier work, and that usually happens in the cloud.
Machine data is only half the picture. Orders, stock levels, and schedules live in MES and ERP systems, and planning tools pull from both before committing to a schedule.
A digital twin in manufacturing is a live software model of a machine or a line, fed by live sensor data. Engineers test a speed change on the twin first, and only touch the real line when the twin says it holds.
The Main Uses of AI on the Factory Floor
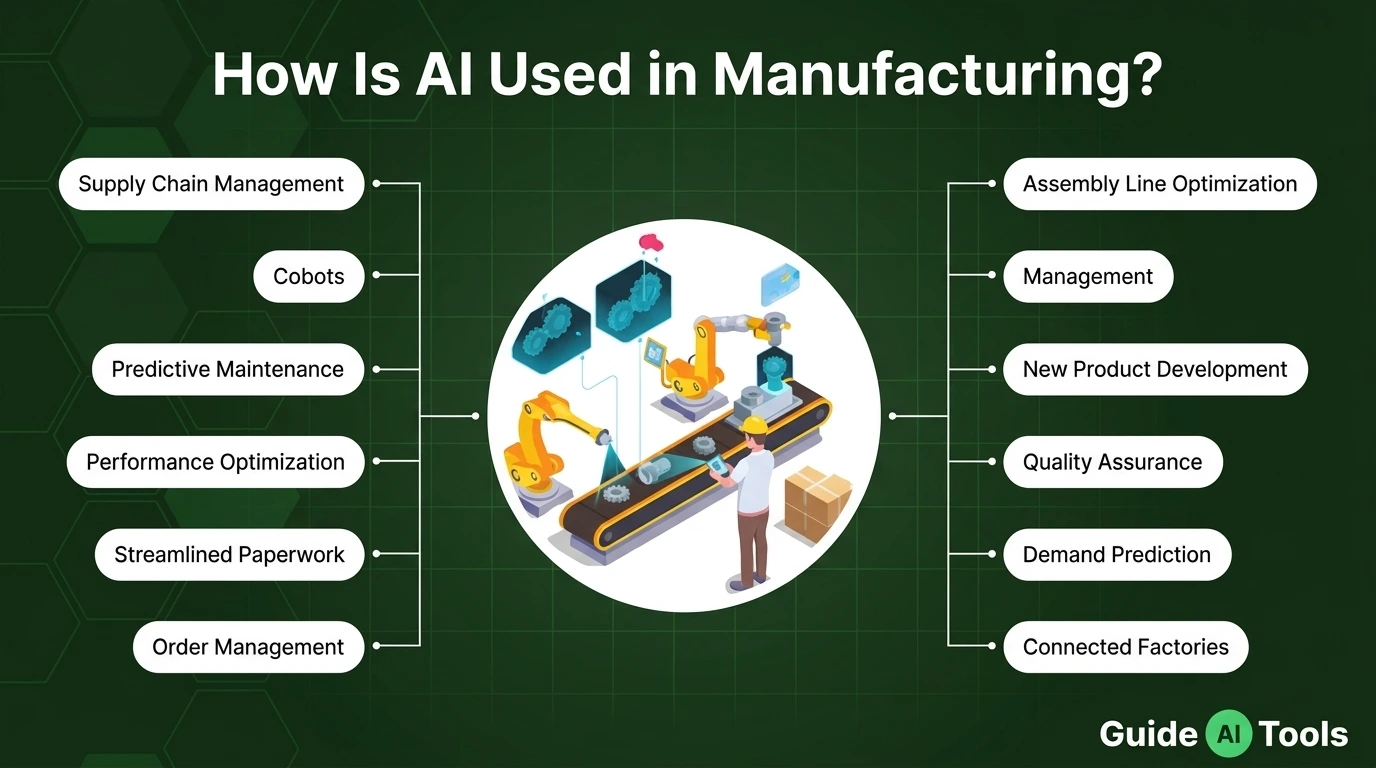
Eight uses cover most of what plants actually run today. Each names the job, the data it feeds on, and the catch.
Predictive maintenance and machine health
Plants handle upkeep three ways. Reactive maintenance fixes a machine after it breaks. Preventive maintenance services it on a calendar, worn or not.
Predictive maintenance watches the machine itself. Vibration, heat, and current data, matched against past failures, flag a bearing or motor days before it fails. Prescriptive systems go further and recommend the fix and the parts.
A model cannot predict a failure it has never seen examples of.
Quality inspection with computer vision
Cameras check every part at full line speed, not one part in fifty. The system flags surface scratches, missing parts, bad stitching, wrong alignment, and parts outside their tolerance. It learns from labeled images of good and bad parts, which is why what computer vision is matters here.
The honest catch: false rejects. A model set too tight scraps good parts, and every plant tunes that line by hand.
Process control and yield
Some models watch the process itself. They read temperature, pressure, and speed, then nudge settings in small steps so output stays inside spec.
A food line holds moisture steady. A press holds thickness steady. Scrap falls because fewer batches drift out of range.
The limit shows up when materials change, and yesterday settings stop fitting today’s input.
Robotics and cobots
Robots are not new on factory floors. What is new is the vision and judgment they carry.
A cobot with a camera finds parts in a bin instead of a fixed tray, guides itself to each one, and works beside people without a cage. AMRs carry material between stations on routes they adjust themselves.
Messy, varied tasks still beat them. Tidy repetition is where they earn their keep.
Production planning and scheduling
Schedulers once rebuilt the plan by hand every time a machine went down. AI planning tools weigh orders, machine availability, and material timing, then reshuffle the day when a line slips.
Newer AI agents draft the revised schedule and the customer updates that go with it, the same pattern reshaping AI in customer service. A person still approves the plan before it reaches the floor.
Supply chain and demand forecasting
Forecasting models read sales history, open orders, and seasonal patterns to warn about shortages weeks earlier than a spreadsheet would. Plants hold less spare stock and still cover demand.
The same forecasting feeds trucks and warehouses, covered in our guide to AI in transportation. And when a campaign lifts demand, the forecast works only if it hears about it, a handoff we cover in AI in marketing.
Forecasts fail hardest when the market jumps without warning.
Generative design and product engineering
Design software can propose part shapes a human would never sketch. The engineer sets the loads, the material, and the space the part must fit, and the software grows a lighter shape that still holds.
Additive printing then builds shapes no mill could cut. The same idea reaches back into the lab, where AI in scientific research helps find new materials worth testing.
Energy and waste reduction
Energy data tells on a plant. Models spot machines left idling overnight, compressed air leaks that hiss money away, and batches that burn power after a setting drifted.
None of it is glamorous. It is often the fastest payback in the building, because the waste was already being paid for.
| Use case | Data it needs | What it replaces | Main limit |
|---|---|---|---|
| Predictive maintenance | Sensor history, failure records | Calendar based servicing | Needs failure examples to learn from |
| Vision inspection | Labeled defect images | Sample checks by eye | False rejects scrap good parts |
| Process optimization | Process settings, output quality | Fixed settings per recipe | Drifts when materials change |
| Robotics and cobots | Cameras, task training | Fixed path automation | Struggles with messy, varied tasks |
| Planning and scheduling | Orders, MES and ERP data | Spreadsheet planning | Bad input data, bad schedule |
| Demand forecasting | Sales and order history | Gut feel ordering | Fails on sudden market shifts |
One connection deserves a name: the defect to machine health loop. When vision inspection sees one defect type creeping up, that trend often means a tool is wearing or a fixture is drifting, long before the machine sounds wrong.
Defect trends are often the first warning that a machine is drifting. Plants that route inspection data to the maintenance team catch the machine problem and the quality problem in one move.
The Benefits Plants Actually Report
Ask plants what changed and the answers repeat. Fewer unplanned stops. Defects caught at the station instead of at the customer audit.
Less scrap, less rework, and staff moved from checking parts to judging calls. The wider benefits of AI show the same shape in other industries.
The figures need care, because most come from the people selling or deploying the systems. McKinsey research on predictive maintenance puts the potential cut in machine downtime at 30 to 50 percent, with maintenance costs down 10 to 40 percent. Treat those as reported ranges from strong adopters, not a promise for your floor.
At GuideAITools, we read vendor numbers like a used car ad. The direction is usually real. The size depends on your baseline, your data, and who owns the project after the demo.
| Metric | Reported effect | Source type |
|---|---|---|
| Unplanned downtime | Down 30 to 50 percent with predictive maintenance | Analyst research, McKinsey |
| Maintenance cost | Down 10 to 40 percent | Analyst research, McKinsey |
| Product waste | About 10 percent powder savings potential reported at Nestle | Vendor case study, AVEVA |
| Defect detection | Above 99 percent reported on trained defect types | Vendor case studies |
The Limits: Where Factory AI Falls Short
Every failure mode in this section has the same root. The model believes its data completely. Feed it a mislabeled defect, a sensor that drifted last spring, or a log with gaps, and it will make confident calls on a false picture. That false confidence is the factory version of AI hallucinations, and it costs parts instead of words.
Old machines are the next wall. An analog press from 1998 produces no data at all until someone retrofits sensors onto it.
A retrofit can add ears and eyes. It cannot fix worn mechanics, and it cannot create the failure history a model needs to learn from.
Then come the two failures operators meet first. False rejects scrap good parts until someone loosens the model. Alert fatigue does the opposite damage: a dashboard that cries wolf daily teaches the crew to ignore it, and the real warning lands in a pile of noise.
Models also drift. Change the product, the material, or the season, and patterns the model learned stop matching the floor. Add pilot purgatory, the demo that impressed everyone and never reached a second line because nobody owned it, and you have the two quiet killers of factory AI.
Money and people close the list. Sensors, integration, and training cost more than the software license, and staff who can run a line and a model are scarce. Every connected machine is also a door into the network, the risk we cover in AI in cybersecurity.
This is why standards work matters, including the NIST artificial intelligence for manufacturing research program, which builds shared metrics for trustworthy AI in plants. The wider pattern sits in our guide to the risks of AI.
How Factories Actually Get Started
Start smaller than the sales pitch. Pick one line and the problem that costs you most, a bottleneck machine or a defect your customers keep finding.
Before you buy anything, record your baselines for a month:
- Unplanned stops per month on that line
- Scrap rate, and what the scrap costs you
- False reject rate at inspection
- Changeover time between products
Then retrofit sensors on the few machines that stop the line most, and run a pilot for 8 to 12 weeks. Give it a named owner and a pass mark written down in advance. Keep people reviewing every AI call during the pilot, because the pilot is where the model earns trust or loses it.
Pass it, and you connect the pilot to your MES and plan line two. Fail it, and you have spent weeks, not a budget year, finding out.
Running a 20 person job shop? Skip the plant wide platform pitch entirely.
Start with vision inspection on your costliest defect, or maintenance alerts on the one machine everything waits for. At GuideAITools, that is the size of first step we would defend in any plant.
FAQs
What is AI in manufacturing in simple terms?
It is software that learns from the data your machines and cameras already produce. It uses those patterns to warn you before a breakdown, check every part for defects, and plan production.
People still run the plant. The software just sees more, and sees it sooner.
How does predictive maintenance work?
Sensors track vibration, heat, and power draw on a machine while it runs. A model compares that stream with patterns from past failures.
When the pattern starts to match, it raises a work order days ahead, and the crew fixes it during a planned stop instead of a breakdown.
What is a smart factory?
A smart factory is a plant where machines, sensors, and software share data as production runs. Orders flow in, machines report their state, and systems adjust schedules and flag problems.
It is a level of connection more than a single product, and most plants get there one line at a time.
Can AI work with old factory machines?
Yes, within limits. Bolt-on sensors can give an old machine a voice, reporting vibration, temperature, and run time.
What a retrofit cannot give it is a recorded failure history, and predictive models learn from history. Expect monitoring and alerts first. Full prediction takes time and data.
Will AI replace factory workers?
It replaces tasks before it replaces people. Checking every part by eye, watching gauges, and rebuilding schedules are tasks software now absorbs.
Setting up machines, judging odd cases, and fixing what breaks still need people. Plants adopting AI move staff toward that work, though the mix of jobs does change.
How much does AI in manufacturing cost?
There is no honest single figure, because the parts differ. You pay for sensors and fitting, integration with your systems, a software subscription, and training for the crew.
The software is often the smallest part. Any vendor who quotes a total before seeing your line is guessing.
What are the disadvantages of AI in manufacturing?
The main ones are cost, data quality, and false alarms. Models trained on messy data make messy calls, inspection systems scrap some good parts, and dashboards that alert too often get ignored.
Add a skills gap and new security risks from connected machines, and the case for starting small writes itself.
Conclusion
So here is your decision. This week, pick the machine that stops your line most, or the defect that costs you most, and measure it for a month before you buy anything.
That baseline tells you whether AI can pay in your plant, and it costs you nothing but attention. Then browse the GuideAITools categories to see the tools behind these use cases, and read the sibling guides in this series as they land.
Related Blog Posts